A concrete mixer drum not turning is more than a truck problem. It can hold up a scheduled pour, leave material setting in the barrel, disrupt dispatch, and turn one disabled unit into an expensive jobsite delay. The fastest way back to production is identifying whether the failure is in the hydraulic drive, electrical controls, PTO system, or drum equipment before parts are replaced blindly.
Start With Safety and the Jobsite Situation
Do not place hands, tools, or clothing near the drum, rollers, drive components, or hydraulic lines while the truck is running. A mixer system can move without warning when a stuck control, electrical short, or hydraulic fault changes state. If concrete is already loaded, notify dispatch immediately and document the load time. The repair priority may change based on how close the material is to setting and whether the truck can safely reach a washout area.
Operators can provide useful first observations without attempting a repair. Note whether the drum stopped suddenly or slowed down, whether it will rotate in one direction but not the other, and whether the engine, PTO, and cab controls appear normal. Also look for hydraulic oil under the truck, damaged wiring around the mixer controls, unusual noise from the pump or motor, and warning lights on the dash.
Why a Concrete Mixer Drum Is Not Turning
Most mixer drum failures fall into four connected systems: the PTO and pump drive, the hydraulic circuit, the electrical control circuit, and the mechanical drum drive. A fault in one system can look like a problem in another. For example, a hydraulic motor that does not turn may have failed internally, but it may also be receiving no oil because the PTO did not engage or a solenoid never received power.
PTO or Pump Drive Failure
On many mixer trucks, the transmission PTO powers the hydraulic pump that supplies the drum motor. If the PTO does not engage, the pump cannot build the flow needed to rotate the drum. The problem may be a failed PTO switch, air supply issue, electrical interlock, damaged wiring, low transmission fluid, or a mechanical PTO failure.
A technician will verify PTO engagement rather than assuming the indicator light tells the whole story. A light can come on even when the PTO is not fully engaged, and a PTO may engage while the hydraulic pump or coupling has a separate mechanical failure. Grinding, rattling, or a sudden loss of drum movement after a driveline noise needs prompt attention to prevent more extensive damage.
Hydraulic Pressure, Flow, or Oil Problems
The hydraulic system is often the first place to investigate when the engine runs normally and the drum controls respond but the barrel will not move. The pump creates flow, control valves direct that flow, and the hydraulic motor converts it into drum rotation. A failure anywhere in that path can stop production.
Low hydraulic oil, an external leak, a collapsed suction hose, a plugged filter, or air entering the system can prevent the pump from delivering proper flow. A worn pump may produce insufficient pressure, particularly when the oil is hot. A relief valve stuck open can bypass oil instead of sending it to the drum motor. A failed directional control valve can prevent rotation in either charge or discharge.
Heat is an important clue. Hydraulic oil that is unusually hot, foamy, dark, or burnt-smelling points to a condition that should be diagnosed before the truck is sent back out. Continuing to run a hydraulic system with low oil or a restricted suction path can turn a repairable fault into pump and motor damage.
Electrical Controls and Interlocks
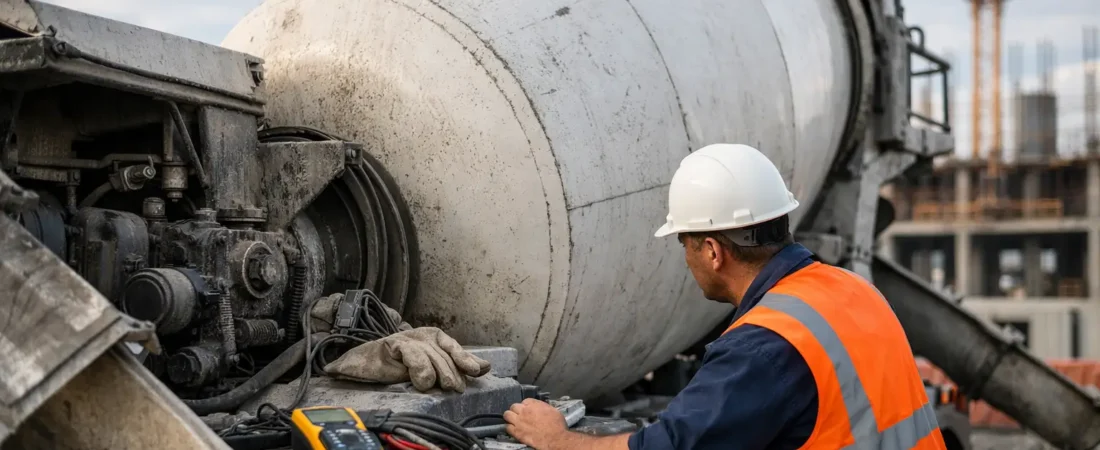
Mixer trucks rely on electrical signals for PTO engagement, remote controls, control-valve solenoids, safety interlocks, and sometimes electronic engine-speed control. Corroded connectors, failed relays, blown fuses, broken control wires, weak grounds, and damaged handheld controls are common reasons a drum stops responding.
Houston-area heat, vibration, moisture, and jobsite contamination are hard on wiring. A wire can look intact until it is tested under load. That is why checking for voltage alone is not always enough. Accurate electrical troubleshooting verifies power, ground quality, command signals, continuity, and voltage drop at the actual component.
If the drum works from one control station but not another, the hydraulic drive may be healthy and the problem may be isolated to a switch, remote pendant, harness, or connector. If it will not rotate in either direction from any station, the diagnostic process needs to include the PTO, pump, control valve, and main power supply.
Mechanical Drum Drive Problems
Not every no-turn condition is hydraulic or electrical. The drum can be mechanically restricted by damaged rollers, seized bearings, broken drive components, a failed gearbox where equipped, or material buildup that has hardened inside the barrel. Unusual banging, metal debris, visible roller damage, or a drum that tries to move but immediately binds are serious warning signs.
A hydraulic motor can also fail mechanically. Internal damage may allow oil to bypass without producing useful torque, or the motor output connection may be damaged. Measuring hydraulic pressure and flow while observing the drive components helps separate a motor problem from a pump or control problem.
A Practical Diagnostic Sequence
Replacing a pump, motor, or valve based on a guess is costly and can leave the actual fault unresolved. A proper field diagnosis follows the power path from the driver’s command to drum movement. That process typically includes four checks:
- Confirm the truck has the required engine operation, transmission condition, PTO engagement, and air or electrical supply.
- Inspect hydraulic oil level and condition, then check hoses, fittings, filters, pump operation, pressure, and flow.
- Test the mixer control circuit for command signals, fused power, relays, grounds, solenoids, connectors, and wiring damage.
- Inspect the motor, drive connections, rollers, drum supports, and any evidence of binding or internal material buildup.
The order matters. A no-crank condition, engine derate, low system voltage, or PTO interlock fault can prevent drum operation even though the mixer equipment itself is in good condition. Likewise, a truck with an active engine or emissions issue may not maintain the speed needed for hydraulic performance. Looking at the truck and mixer as one operating system avoids repeat downtime.
What Operators Should Avoid
Do not increase engine RPM aggressively in an attempt to force a nonresponsive drum to move. If the pump is starved, a line is restricted, or the motor is binding, higher RPM can increase heat and damage. Avoid repeatedly cycling a PTO that is grinding or will not stay engaged.
Do not loosen hydraulic fittings to check for pressure. High-pressure hydraulic fluid can penetrate skin and cause a medical emergency, even through gloves. A suspected hydraulic leak or pressure issue requires the right gauges, test equipment, and safe procedures.
It is also risky to keep driving a loaded mixer if the drum cannot rotate. Concrete may begin setting, the load can become unusable, and hardened material can create a far larger cleanup and repair expense. Dispatch decisions should account for material time, road safety, available washout options, and the condition of the truck.
When Mobile Mixer Truck Repair Makes Sense
A mobile heavy-duty technician can often diagnose a stopped drum at the yard, jobsite, or roadside without the added delay and cost of towing a mixer truck. This is especially valuable when the truck is loaded, the fault involves wiring or controls, or the repair requires hydraulic and diesel troubleshooting together.
AP Diesel Diagnostics provides on-site diagnostic support for mixer-truck hydraulic, electrical, PTO, engine-performance, and related equipment faults in Houston and surrounding areas. Field testing can identify whether the repair is a failed solenoid, damaged harness, PTO issue, hydraulic restriction, pump problem, motor failure, or mechanical binding before unnecessary major components are ordered.
The right repair depends on what failed and why. A worn hydraulic pump, for example, may be the immediate problem, but contaminated oil or a restricted suction line may have caused the failure. Correcting only the pump can put the truck back into service briefly, then create another breakdown when the underlying cause remains.
A stopped drum demands quick action, but the best recovery is controlled, safe, and evidence-based. Get the load situation under control, keep people clear of moving and pressurized components, and have the entire mixer drive system tested so the truck returns to work with a repair you can rely on.